For India's steel plants, cement majors & machine-tool builders
Heavy Engineering Castings Built With Precision. Designed To Perform.
Mill housings, slag pots, kiln tyres, machine-tool beds — single-piece, certified, INR-priced. The casting lands ready to install, not ready to argue about.
About Bhawani
India's answer to the import order.
Bhawani Industries is the Heavy Engineering Casting division of the Royal Group. Pattern, melt, cast, heat-treat, machine and test all happen on one 55-acre site in Mandi Gobindgarh — under an owner who signs off every heat that ships.
Read the full story →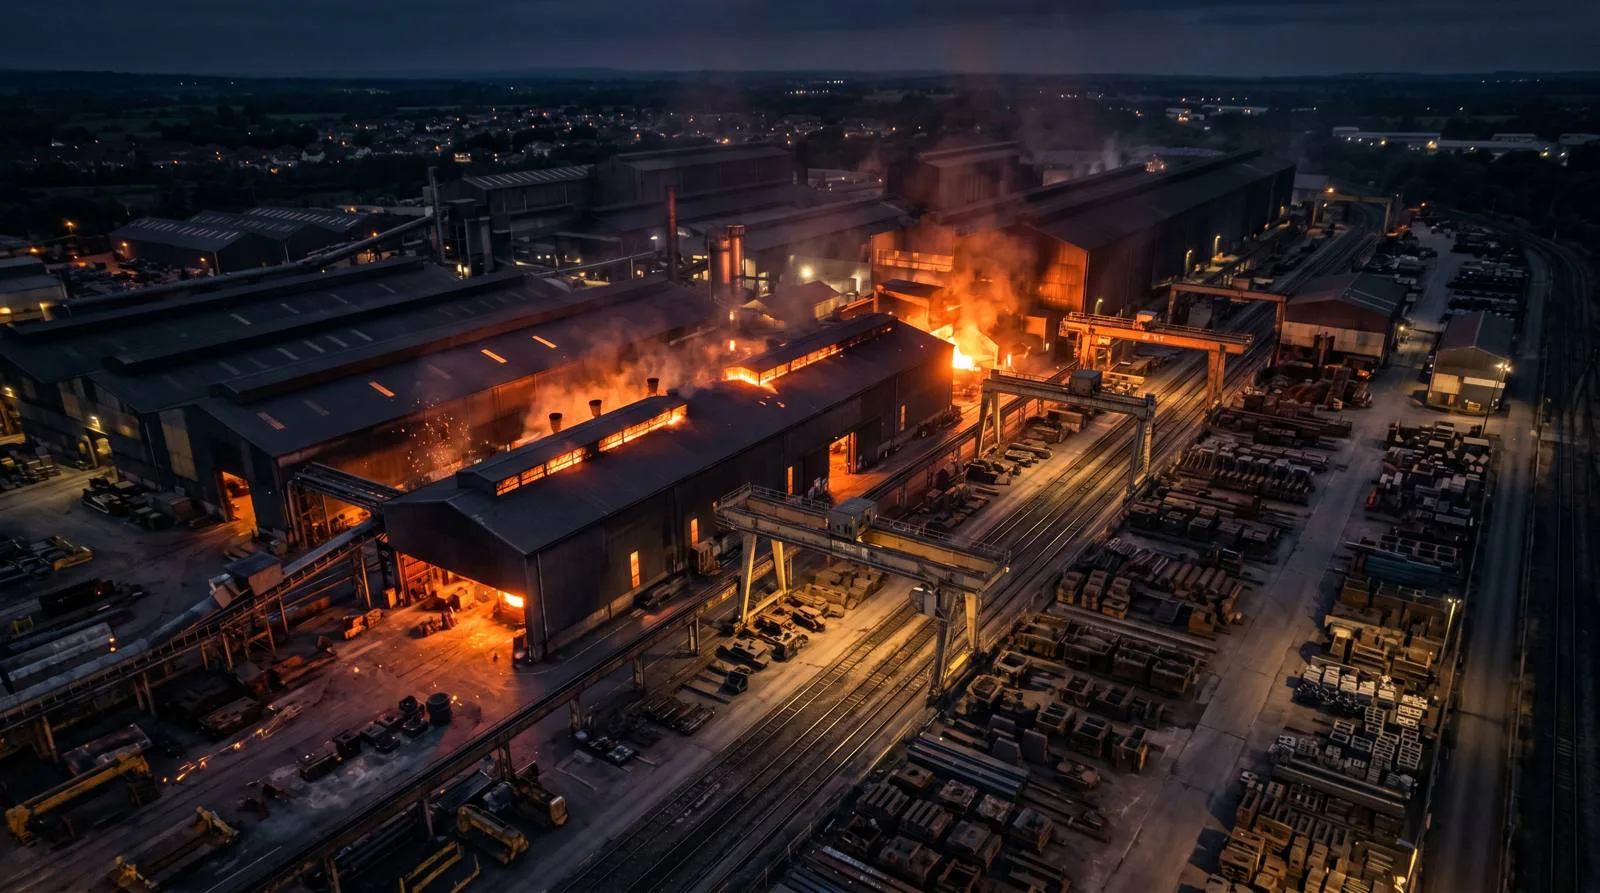
The names that already specify Bhawani castings
Cast for the plants that set the standard.
The casting envelope
Six core castings.
One foundry.
Six core castings under one accountable signature — each engineered to the duty cycle, not pulled from a catalogue.
Where Bhawani castings work hard, every shift
Eight industries served.
Integrated Steel Plants
Hot & cold rolling lines, meltshops and caster bays — mill housings, chocks and slag pots.
Machine-Tool Builders
Large structural and VTL castings — beds, columns and cross rails to 10 m.
Steel Plant OEMs
Whole casting sets, pattern to dispatch — supplied proof- or finish-machined to drawing.
Sponge Iron Plants
Heavy-section wear and structural parts built for abrasive, high-temperature duty.
Power Generation
Turbine casings, hydro runners and heavy rotating components in pressure-grade steel.
Cement Plants
Kilns, grinding circuits and mill internals — tyres, support rollers and grinding tables.
Heavy Engineering
Forging-press anvils, ingot moulds and structural castings for capital plant.
Sugar & Process Plants
Heavy rotating and static castings engineered to the duty cycle, not the catalogue.
The Five-Point Lifecycle Audit.
Most plants accept short casting life as the cost of doing business. It isn't. Bring your service-life data; we'll show you exactly where the money is leaking — landed price is rarely where it hides.
Your service-life log
Per-asset failure history · the spec on the current drawing · what each replacement cycle costs you. No prep on your side.
A cost-per-tonne analysis
Failure modes mapped to metallurgical fixes · true cost-per-tonne-handled · a spec-tightening loop. Yours to keep, supplier-agnostic.
30–40% lower cost-per-tonne
What plants applying this framework report within 18–24 months. It transfers to housings, chocks and kiln tyres alike.
Prefer to read first? Download the 12-page briefing →
Proof points the foundry has earned
Six milestones. Each still in service.
India’s first single-piece mill housing at this weight
Cast, heat-treated and stress-relieved in-house, delivered to an integrated steel-plant rolling mill.
A housing China quoted at 30 weeks — delivered in 18
North-India proximity, no customs, no freight risk. The lead time the import route structurally can't match.
Slag pots crossing 7 years against a 10-year spec
An SMS plant whose previous pots lasted four. The campaign on the Bhawani replacements isn't over yet.
Supplied casting for India's largest gantry mill
Beds, columns and cross rails supplied complete to an Indian machine-tool builder.
Supplied casting for India’s biggest VTL with cross rail spanning 16 meters in length
Exporting across SE Asia, Gulf, Africa, LatAm, USA & EU
Showcased at METEC / GIFA 2023, Dusseldorf — the global heavy-casting benchmark show.
In the words of the people who run the castings
What plant heads tell us, six months in.
"Pattern shop in-house. Machine shop in-house. We stopped chasing three vendors for one casting — that's the real saving, not the line price."
Steel Plant OEM
"When a chock spec was questioned, the foundry head was on the call the same day. Try getting that from a sales desk three time-zones away."
Integrated Steel Plant · East India
"Their test certificate matched our witnessed inspection to the decimal. We've stopped re-testing Bhawani castings on receipt."
Cement Major · West India
The person who picks up your call
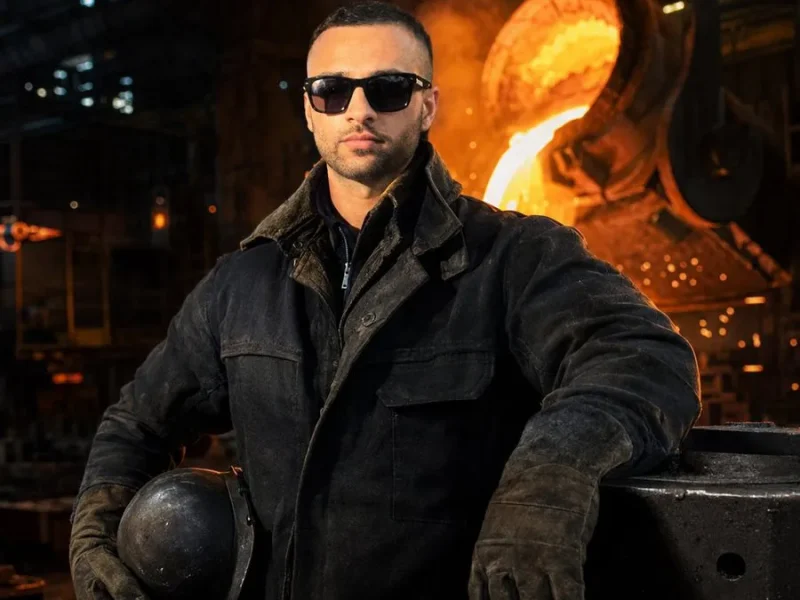
Naman Sood. Fourth generation on the floor.
Naman Sood is the technical custodian of the Bhawani foundry — the engineer who personally owns the hardest pours and the toughest specs on the floor.
Customers don't pass through a sales layer. They speak to Naman or his engineering team directly: specs are debated, failure modes interrogated, and the casting that ships is the one both sides committed to. When a casting is questioned, he's the one who answers.
Questions procurement teams ask before the first call
Frequently asked, honestly answered.
12–18 weeks depending on the order. We hold spare capacity for emergencies — a critical casting can be put on our priority "ambulance" lane and fast-tracked ahead of the queue on an emergency basis.
None. We accept single-piece orders. Repeat-spec batches attract a pricing benefit.
Yes — proof- or finish-machined to your drawing, in-house.
Anchor accounts are shown on the client wall above. Project-specific approval letters shared on request.
Encouraged. Half-day tours cover melt shop, foundry, heat treatment, machine shop and lab. Five hours from Delhi.
Advance against pattern, balance against pro forma or LC on dispatch. Negotiable with vendor rating.
Yes — we export regularly and ship to demanding international buyers. Recent showcases on request.
The next step is small
Send the
drawing.
Most heavy-casting decisions die in a six-month silence. Ours is the opposite. Share a component drawing or a service-life problem — within five working days you'll have a written response: feasibility, indicative timeline, and the two or three questions whose answers change the casting.
When the casting decision can't wait
Emergency replacement escalation
Choose the ambulance route
Heavy castings fail at the worst possible moments — mid-campaign, mid-pour, mid-shift. Bhawani holds spare capacity for exactly that: an emergency casting takes the ambulance route through the plant and is prioritised over scheduled work. If a campaign-critical casting fails, your first email should go to:
Identify casting type, weight class, plant location and required dispatch date in the first message. Expect a held-stock availability confirmation within four working hours during plant hours.